Food Manufacturing: Best Practices and Complete Guide
Explore essential food manufacturing practices, technologies, and strategies. Learn how modern facilities maintain quality, safety, and efficiency in production processes.
Food manufacturing is a complex and highly regulated industry that bridges agriculture and consumer markets. Modern food production facilities must balance efficiency, safety, quality, and sustainability while meeting strict regulatory standards. Understanding the fundamentals of food manufacturing helps stakeholders make informed decisions about operations, investments, and process improvements. This comprehensive guide explores the essential practices, technologies, and strategies that define successful food manufacturing operations in today's competitive landscape.
Understanding Food Manufacturing Fundamentals
Food manufacturing encompasses the transformation of raw agricultural materials into finished products ready for consumer consumption. This process involves multiple stages including receiving, processing, packaging, and distribution. Each stage requires careful attention to quality parameters, safety protocols, and regulatory compliance. The complexity of food manufacturing varies significantly depending on the product category—from simple grain processing to complex multi-ingredient prepared foods requiring specialized equipment and expertise.
Benefits and Limitations of Modern Food Manufacturing
Modern food manufacturing offers numerous advantages to producers and consumers alike. Standardized processes ensure consistent product quality, extended shelf life, and reliable supply chains. Automation and technology improvements have increased production efficiency while reducing labor costs and human error. Food manufacturing also enables food preservation and distribution to regions where fresh products are unavailable, improving food security globally.
However, food manufacturing also presents significant challenges. High initial capital investment in equipment and facilities can be prohibitive for small producers. Regulatory compliance requires continuous monitoring and documentation. Environmental concerns related to water usage, waste management, and energy consumption demand sustainable practices. Supply chain vulnerabilities, ingredient sourcing challenges, and the need for constant innovation to meet consumer preferences add complexity to manufacturing operations.
Types of Food Manufacturing Operations
Food manufacturing encompasses diverse operational models tailored to different product categories and market segments:
- Beverage Manufacturing: Includes water bottling, juice production, soft drinks, and alcoholic beverages requiring specialized equipment for mixing, carbonation, and pasteurization.
- Meat and Poultry Processing: Involves slaughtering, butchering, curing, and packaging of animal proteins with stringent sanitation and food safety requirements.
- Dairy Processing: Transforms milk into cheese, yogurt, butter, and other products through fermentation, separation, and pasteurization processes.
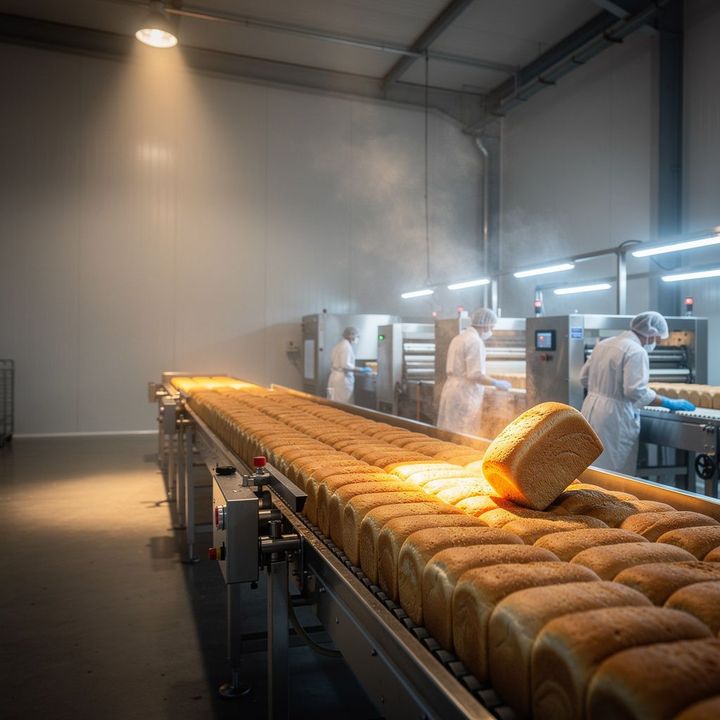
- Grain and Cereal Manufacturing: Processes grains into flour, breakfast cereals, and baked goods using milling, mixing, and baking technologies.
- Prepared Foods and Meals: Combines multiple ingredients into ready-to-eat or ready-to-cook products requiring complex recipe management and quality control.
- Snack Food Production: Manufactures chips, nuts, confectionery, and other shelf-stable snacks using frying, roasting, or coating processes.
Current Industry Trends and Innovations
The food manufacturing sector continues to evolve rapidly in response to consumer demands, technological advances, and regulatory pressures. Plant-based protein manufacturing has emerged as a significant growth area, with facilities developing new technologies to create meat and dairy alternatives. Automation and Industry 4.0 technologies including artificial intelligence, machine learning, and IoT sensors are increasingly deployed to optimize production efficiency and predict maintenance needs.
Sustainability has become a core focus, with manufacturers investing in renewable energy, water recycling systems, and waste reduction technologies. Traceability and transparency technologies, including blockchain applications, enable better tracking of ingredients and products throughout the supply chain. Cold chain innovations improve the distribution of temperature-sensitive products, while packaging innovations focus on reducing environmental impact while maintaining product protection.
Essential Features of Modern Food Manufacturing Facilities
Successful food manufacturing facilities incorporate several critical features:
| Feature Category | Key Components | Purpose |
|---|---|---|
| Quality Control Systems | Testing labs, inspection equipment, documentation systems | Ensure product consistency and safety |
| Sanitation Infrastructure | Cleaning equipment, drainage systems, segregated zones | Prevent contamination and maintain hygiene |
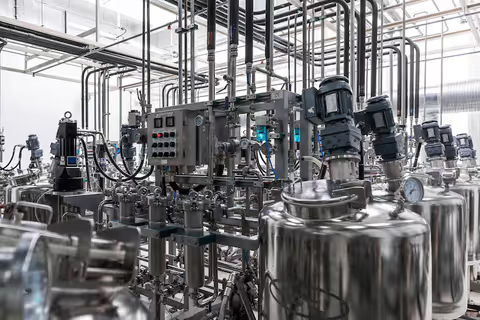
| Processing Equipment | Mixers, ovens, refrigeration, packaging machinery | Transform raw materials into finished products |
| Storage Systems | Temperature-controlled warehouses, inventory management | Preserve product quality during storage |
| Monitoring Technology | Sensors, cameras, data logging systems | Track conditions and detect anomalies |
Leading Food Manufacturing Companies and Models
The global food manufacturing landscape includes multinational corporations operating hundreds of facilities alongside regional producers and artisanal manufacturers. Large-scale manufacturers benefit from economies of scale, advanced automation, and extensive distribution networks. Mid-sized manufacturers often specialize in specific product categories or regional markets, balancing efficiency with flexibility. Smaller manufacturers and co-packing facilities serve niche markets and provide contract manufacturing services for brands without their own production capacity.
Selecting and Implementing Food Manufacturing Solutions
Organizations entering or expanding food manufacturing operations should evaluate several critical factors. Regulatory requirements vary by product type, target market, and ingredient composition—understanding applicable standards is essential before facility design. Production volume projections determine equipment scale and facility size. Ingredient sourcing reliability affects production scheduling and supply chain resilience. Technology infrastructure needs depend on desired automation levels and data collection requirements. Workforce expertise requirements influence hiring and training strategies.
Implementation typically involves facility design and construction, equipment installation and validation, staff training, and regulatory approval processes. Phased approaches allow operators to test processes at smaller scales before full production. Partnerships with equipment suppliers, consultants, and regulatory experts accelerate implementation timelines and reduce risks.
Best Practices for Food Manufacturing Success
Implementing these best practices enhances food manufacturing operations:
- Establish Robust Quality Management Systems: Implement HACCP (Hazard Analysis and Critical Control Points) and other food safety frameworks to identify and control risks systematically.
- Invest in Staff Training: Regular training ensures employees understand food safety, equipment operation, and quality standards, reducing errors and improving consistency.
- Maintain Equipment Properly: Preventive maintenance schedules minimize unexpected downtime and extend equipment lifespan while ensuring optimal performance.
- Document Everything: Comprehensive documentation of processes, testing results, and corrective actions demonstrates compliance and enables continuous improvement.
- Monitor Key Performance Indicators: Track metrics like production efficiency, waste rates, and quality defects to identify improvement opportunities.
- Engage Suppliers: Collaborate with ingredient suppliers to ensure consistency, quality, and traceability of raw materials.
- Embrace Technology: Leverage automation, data analytics, and monitoring systems to improve efficiency and decision-making.
Frequently Asked Questions About Food Manufacturing
What are the main food safety regulations manufacturers must follow?
Food manufacturers must comply with regulations established by agencies like the FDA in the United States, EFSA in Europe, and equivalent bodies in other countries. Key frameworks include HACCP, FSMA (Food Safety Modernization Act), and ISO 22000 standards. Requirements vary by product type and target market, covering areas like sanitation, labeling, allergen management, and traceability.
How do manufacturers ensure product consistency across batches?
Product consistency is maintained through standardized recipes, precise ingredient measurements, controlled processing parameters, and comprehensive quality testing. Modern facilities use automated systems to monitor temperature, time, and other critical variables. Regular calibration of equipment and testing of finished products verify that each batch meets specifications.
What role does automation play in modern food manufacturing?
Automation improves efficiency, consistency, and safety in food manufacturing. Automated systems handle repetitive tasks, reducing labor costs and human error. Sensors and monitoring systems track critical parameters in real-time. Automated packaging lines increase throughput while maintaining precise portion control. However, some specialty products still benefit from manual craftsmanship and artisanal approaches.
How do manufacturers manage allergen control?
Allergen management requires identifying all allergens in ingredients, implementing segregation procedures to prevent cross-contamination, training staff on allergen protocols, and maintaining detailed documentation. Many facilities use dedicated production lines for allergen-free products or schedule allergen-containing products during specific production windows with thorough cleaning between runs.
What sustainability practices are food manufacturers adopting?
Manufacturers increasingly implement water conservation systems, renewable energy sources, waste reduction and recycling programs, and sustainable packaging solutions. Many facilities conduct life cycle assessments to identify environmental impacts and opportunities for improvement. Collaboration with suppliers on sustainable sourcing practices extends environmental responsibility throughout supply chains.
How do manufacturers handle supply chain disruptions?
Resilient supply chains include multiple suppliers for critical ingredients, strategic inventory buffers, and contingency plans for various disruption scenarios. Strong supplier relationships and communication systems enable rapid response to changes. Some manufacturers invest in vertical integration or develop alternative ingredients to reduce dependency on single sources.
Conclusion
Food manufacturing is a sophisticated industry that combines traditional food science with modern technology to deliver safe, consistent, and appealing products to global consumers. Success requires understanding regulatory requirements, implementing robust quality systems, investing in appropriate technology, and maintaining skilled workforces. As consumer preferences evolve and environmental concerns intensify, food manufacturers must balance efficiency with sustainability and innovation. By adopting best practices, embracing technology, and maintaining focus on food safety and quality, manufacturers can build resilient operations that meet current demands while adapting to future challenges. The food manufacturing industry will continue to evolve, offering opportunities for those who understand its complexities and commit to continuous improvement.